We at TAGOOR LABS, are committed to manufacture products in total compliance with cGMP (Current Good Manufacturing Practices) requirements and match customer expectations. All processes and manufacturing operations are in accordance with the regulatory framework established by ICH (Q7). With three decades of manufacturing experience, the company, today has transformed into a multi-ton, multi-location GMP-Certified entity. Our considerably large manufacturing infrastructure helps us to meet the diverse volume requirements efficiently and effectively. The company has the capability and the flexibility to manage projects that range from ‘Grams to Tons’ with rigorous system checks and project control to ensure strict confidentially.
Manufacturing
We at TAGOOR LABS, are committed to manufacture products in total compliance with cGMP (Current Good Manufacturing Practices) requirements and match customer expectations. All processes and manufacturing operations are in accordance with the regulatory framework established by ICH (Q7). With three decades of manufacturing experience, the company, today has transformed into a multi-ton, multi-location GMP-Certified entity.
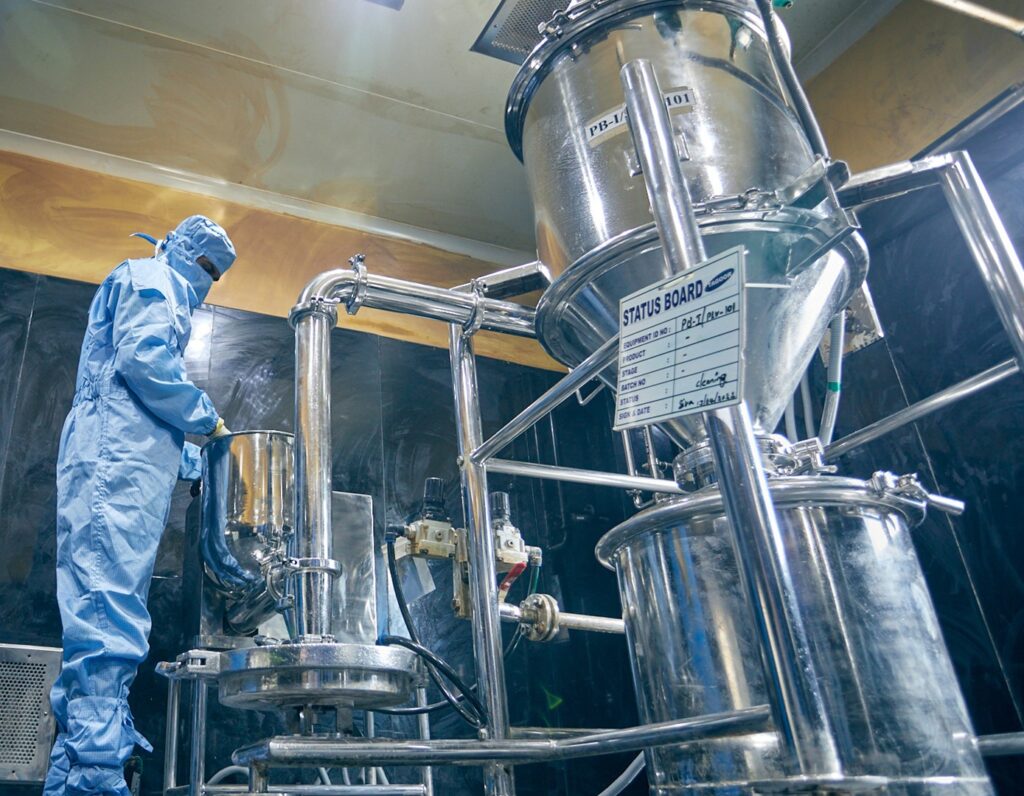
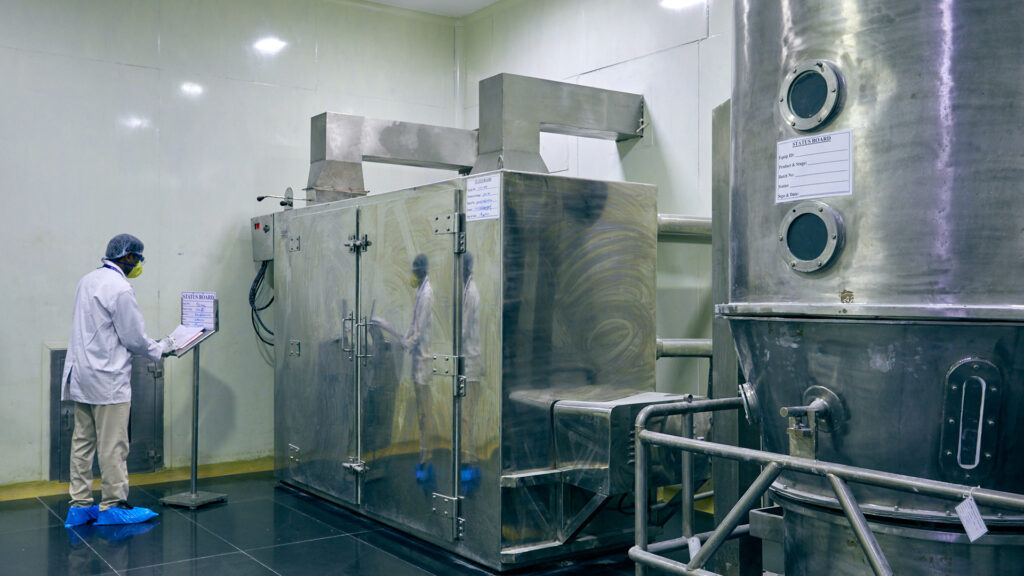
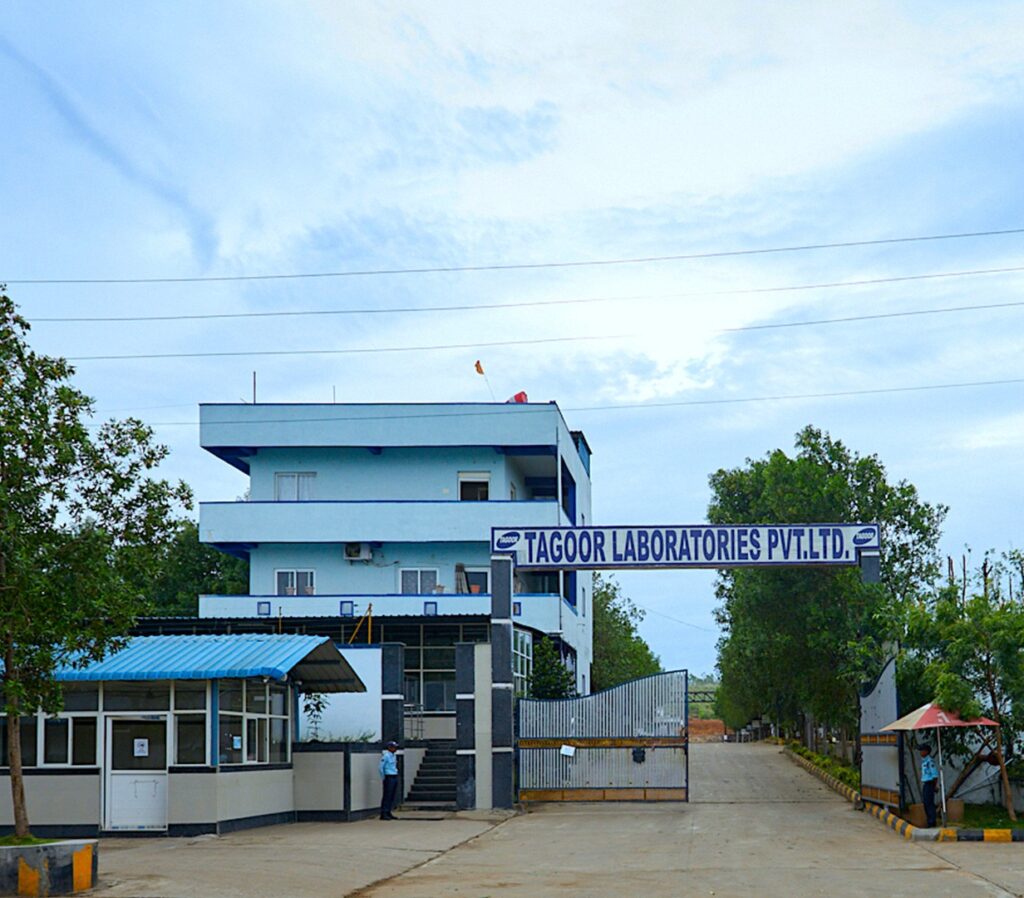
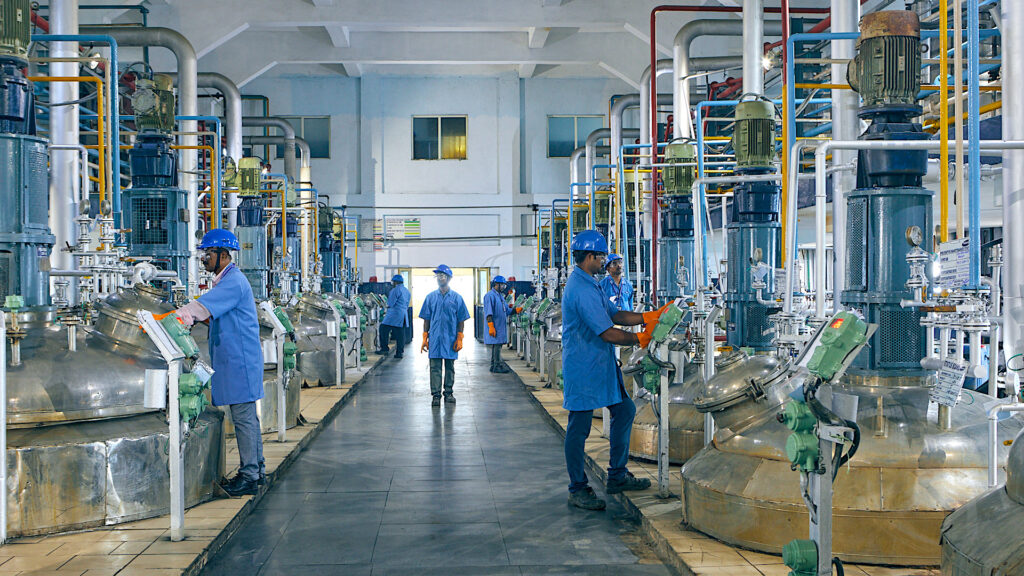
Our three manufacturing facilities equipped with advanced systems are truly state-of-the-art, with each of the facility having a clearly defined purpose and market-orientation, to enable seamless production regimes. These facilities, spread across huge expanse follow stringent quality and regulatory protocols to ensure that the APIs and Intermediates manufactured here are only of the highest quality and purity.
At TAGOOR LABS, we make continuous investments in the upgradation of manufacturing facilities with special emphasis on deploying advanced machinery and adopt latest processes and technologies to ensure that our products not only comply with GMP requirements, but also meet global standards of high quality.
At TAGOOR LABS, we make continuous investments in the upgradation of manufacturing facilities with special emphasis on deploying advanced machinery and adopt latest processes and technologies to ensure that our products not only comply with GMP requirements, but also meet global standards of high quality.
Our Capabilities
Our Capabilities
Manufacturing
Highly experienced manufacturing and engineering team
Robust planning process driven by customer demand
Expertise in handling a wide range of process equipment supporting the chemistries
Wide range of utility equipment to support critical process parameters
Production
Well-equipped GMP compliant facility
Facility designed to manufacture multiple products
Nine clean room modules for different APIs
Multi-reaction facility
Dedicated block for Hydrogenation and Nitration reactions
Reactions
Friedel–Crafts Reactions
Nitration Reactions
Cyanation
Oxidation Reactions
Hydrogenations (Reduction using Raney Nickel, Palladium Catalyst and H2 Gas)
Grignard Reactions
Halogenations using Liquid Bromine and Chlorine Gas
Thermodynamic Rearrangements at High Temperatures (up to 250°C)
Liquid Purification using High Vacuum Distillation
Cryogenic Reactions (up to -80°C)
Highlights of our Infrastructure
Utility Services
Total Reactors Volume: 1500 kL
Reactor Details: Size ranges from 250L to 15000L
Temperature: -80°C to + 200°C
Material of Construction: SS, GL, MSGL
Packing Control: Meet requirements of ISO Class – 8
Cooling Water Tower: 1540 TR
Chilled Water: 247 TR
Purified Water System: 2000 LPH
Hot Water: up to 90°C
Steam: 32 TPH
Vacuum System: up to 1 Torr
Compressed Air: 1170 CFM
Captive Power Generators: 3000 KVA
Fresh Solvent Storage Tank Farm capacity (as per CCOE): 700 kL
Highlights of our Infrastructure
Packaging & Warehousing
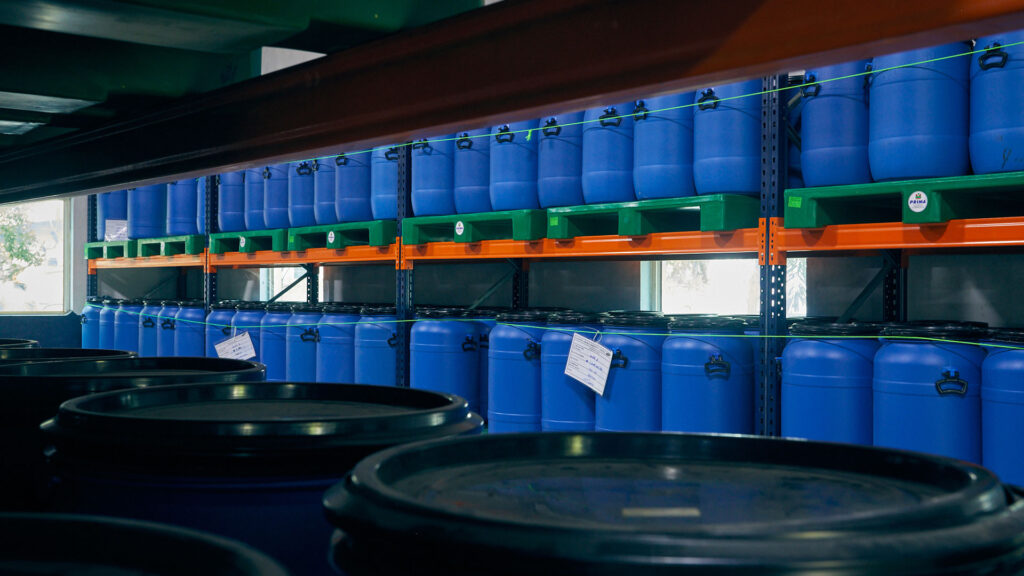
Separate storage facility for Solid and Liquid Raw Materials
Separate area for Packing Material storage
Solid Raw Material storage capacity: 150 MT
Liquid Raw Material storage capacity: 72 kL
Separate dispensing area for Solid and Liquid Raw Material
Separate Quarantine Area, Sampling Room, Washing Area
Controlled temperature storage: +2 to +8 Degree Celsius
Inventory Control & Material Management
Testimonials
Trusted by Pharma Leaders
Global Pharmaceutical Procurement HeadGlobal Pharmaceutical Procurement Head
Partnering with Tagoor Labs has boosted our supply reliability. Their commitment to quality, compliance, and on-time delivery has consistently supported our API needs across multiple therapeutic segments.
Head of R&D, Mid-Sized Pharma CompanyHead of R&D, Mid-Sized Pharma Company
We’ve scaled our production timelines thanks to Tagoor’s strong CDMO capabilities. Their scientific expertise and proactive communication have made them a trusted development partner.
Quality Assurance Lead, International Generics FirmQuality Assurance Lead, International Generics Firm
Tagoor Laboratories’ manufacturing excellence and adherence to stringent global quality standards give us confidence in every batch. Their customer-centric approach sets them apart.
COLLABORATE WITH TAGOOR LABORATORIES
Partner With Us for Pharmaceutical Development & Manufacturing
Whether you require API development, Advanced Intermediates, KSMs, custom synthesis, analytical R&D or CDMO support, Tagoor Laboratories brings together scientific expertise and pharmaceutical manufacturing capabilities to address complex development requirements.
What type of products does Tagoor Labs specialize in?
Tagoor Labs specializes in high-quality APIs, advanced intermediates, and key starting materials, with expertise in complex and multi-step chemical synthesis.
How can I collaborate on a custom synthesis project?
You can collaborate by reaching out to our business development team with your project requirements. We evaluate feasibility, share a development plan, and then proceed with transparent deliverables.
Where are your manufacturing facilities located?
Our cGMP-compliant manufacturing facilities are located in Andhra Pradesh, India, with corporate and R&D offices based in Hyderabad.
Do you offer training or internship programs?
Yes, Tagoor Labs provides training and internship opportunities for qualified candidates in R&D, analytical labs, and manufacturing departments, depending on availability.
Which analytical technologies are used?
We use advanced analytical tools such as HPLC, GC, LC-MS, UV, IR, and other modern instrumentation to support method development, validation, and quality testing.
How can I access published research or certificates?
You can request documentation, COAs, DMFs, and research information directly through our support or business enquiry team, who will share the required files securely.